Two ropes can both contain polymer and still solve very different problems. I often see buyers compare them as if they were the same product.
I choose plastic-coated rope for external surface protection and contact control. I choose plastic-impregnated rope when the application needs reduced internal friction, better strand stability, and improved fatigue performance inside the rope.
A buyer once asked for “PVC wire rope” for a crane. The real need was internal wear control, not a colored cover. One question changed the entire specification.
What Is the Difference Between Plastic-Coated and Plastic-Impregnated Rope?
I start by locating the polymer. Its position tells me what it can protect and what it can hide.
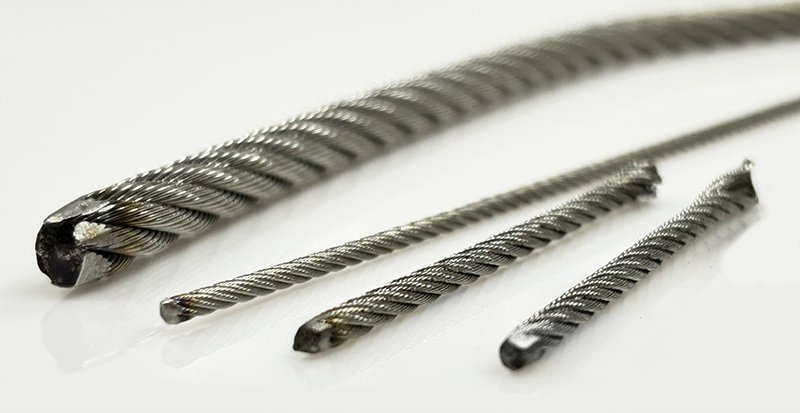
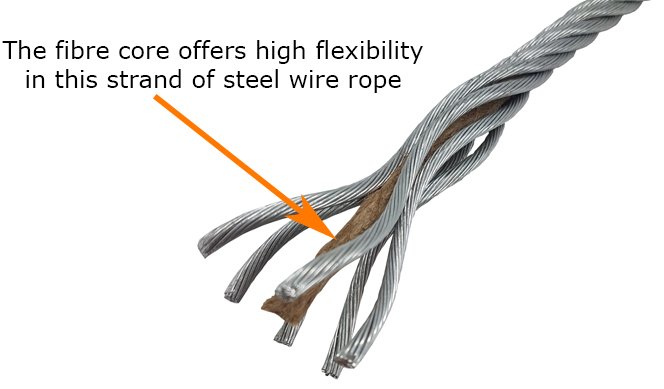
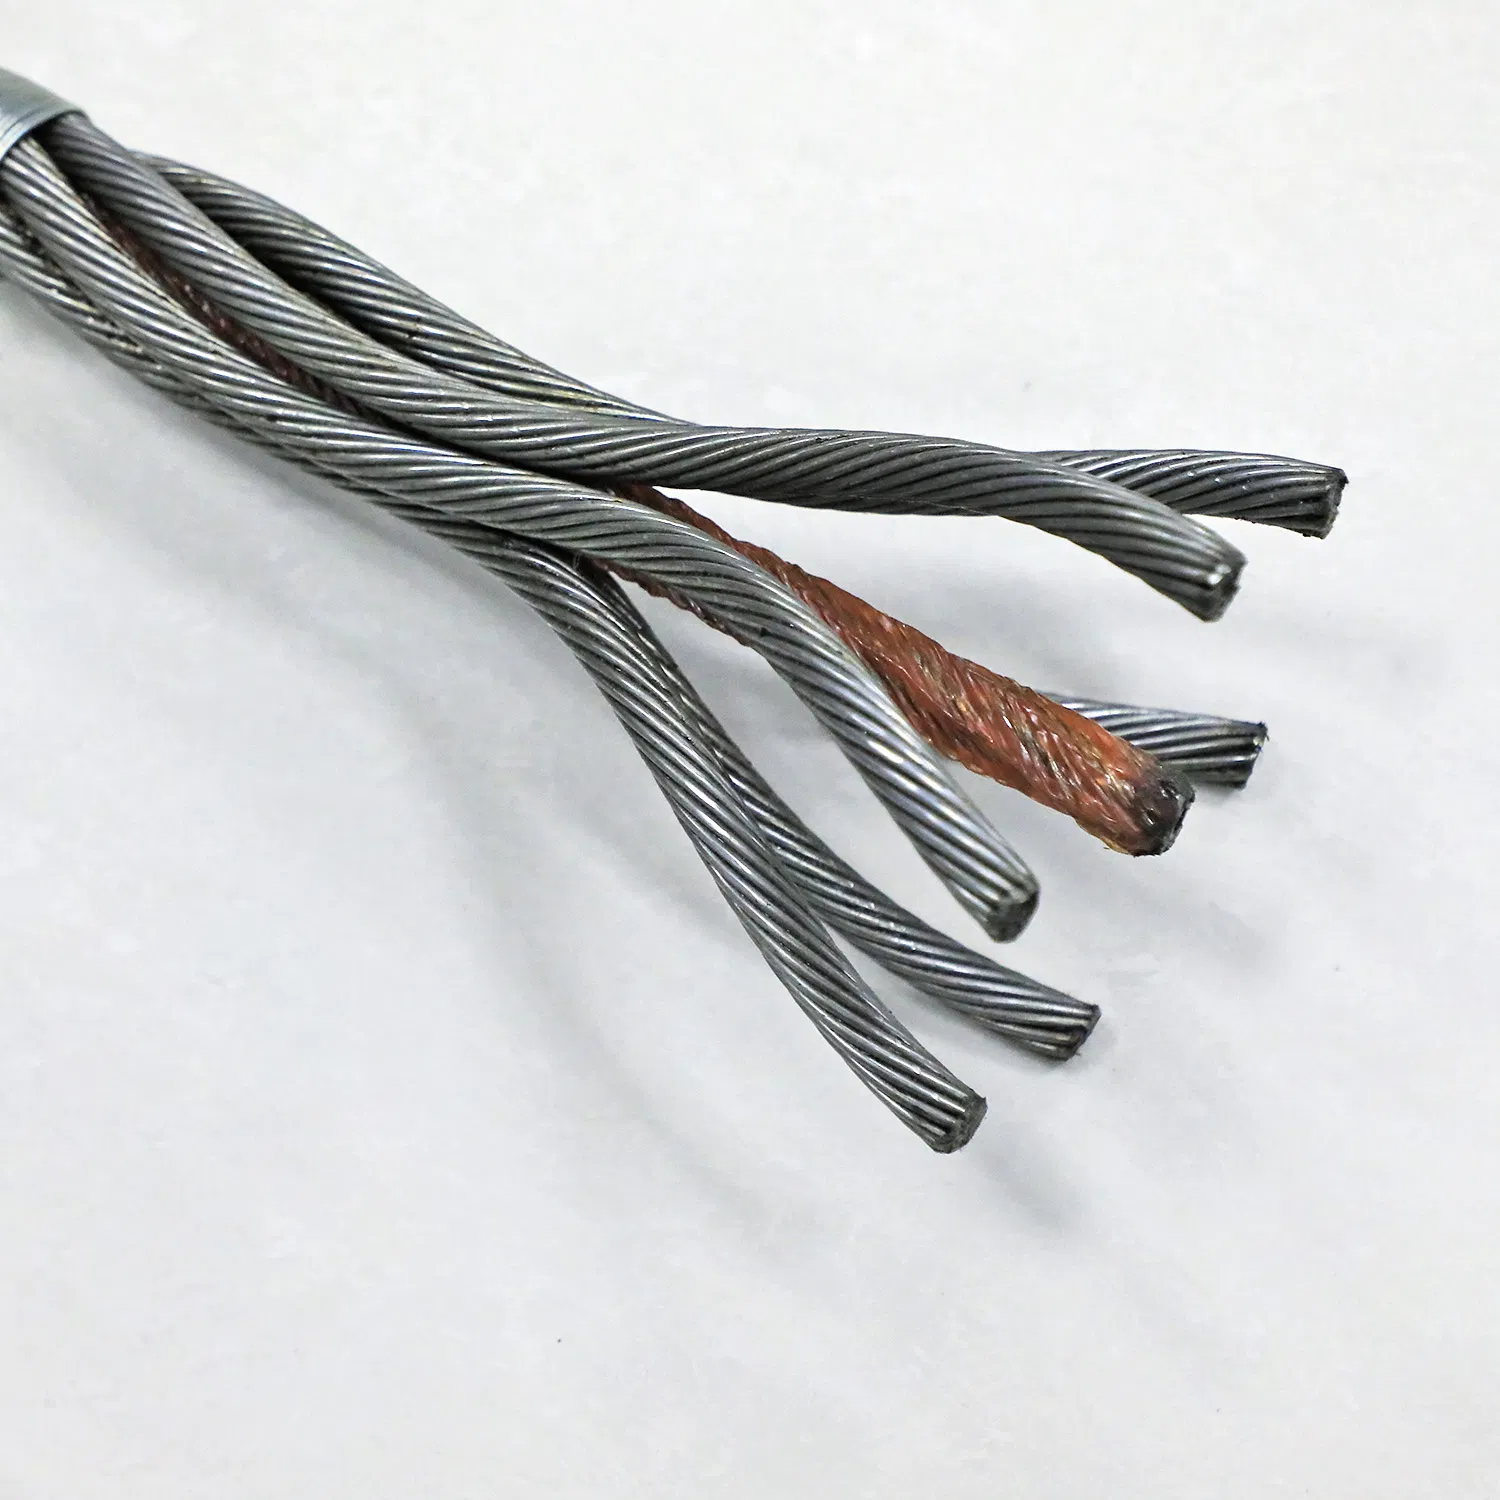
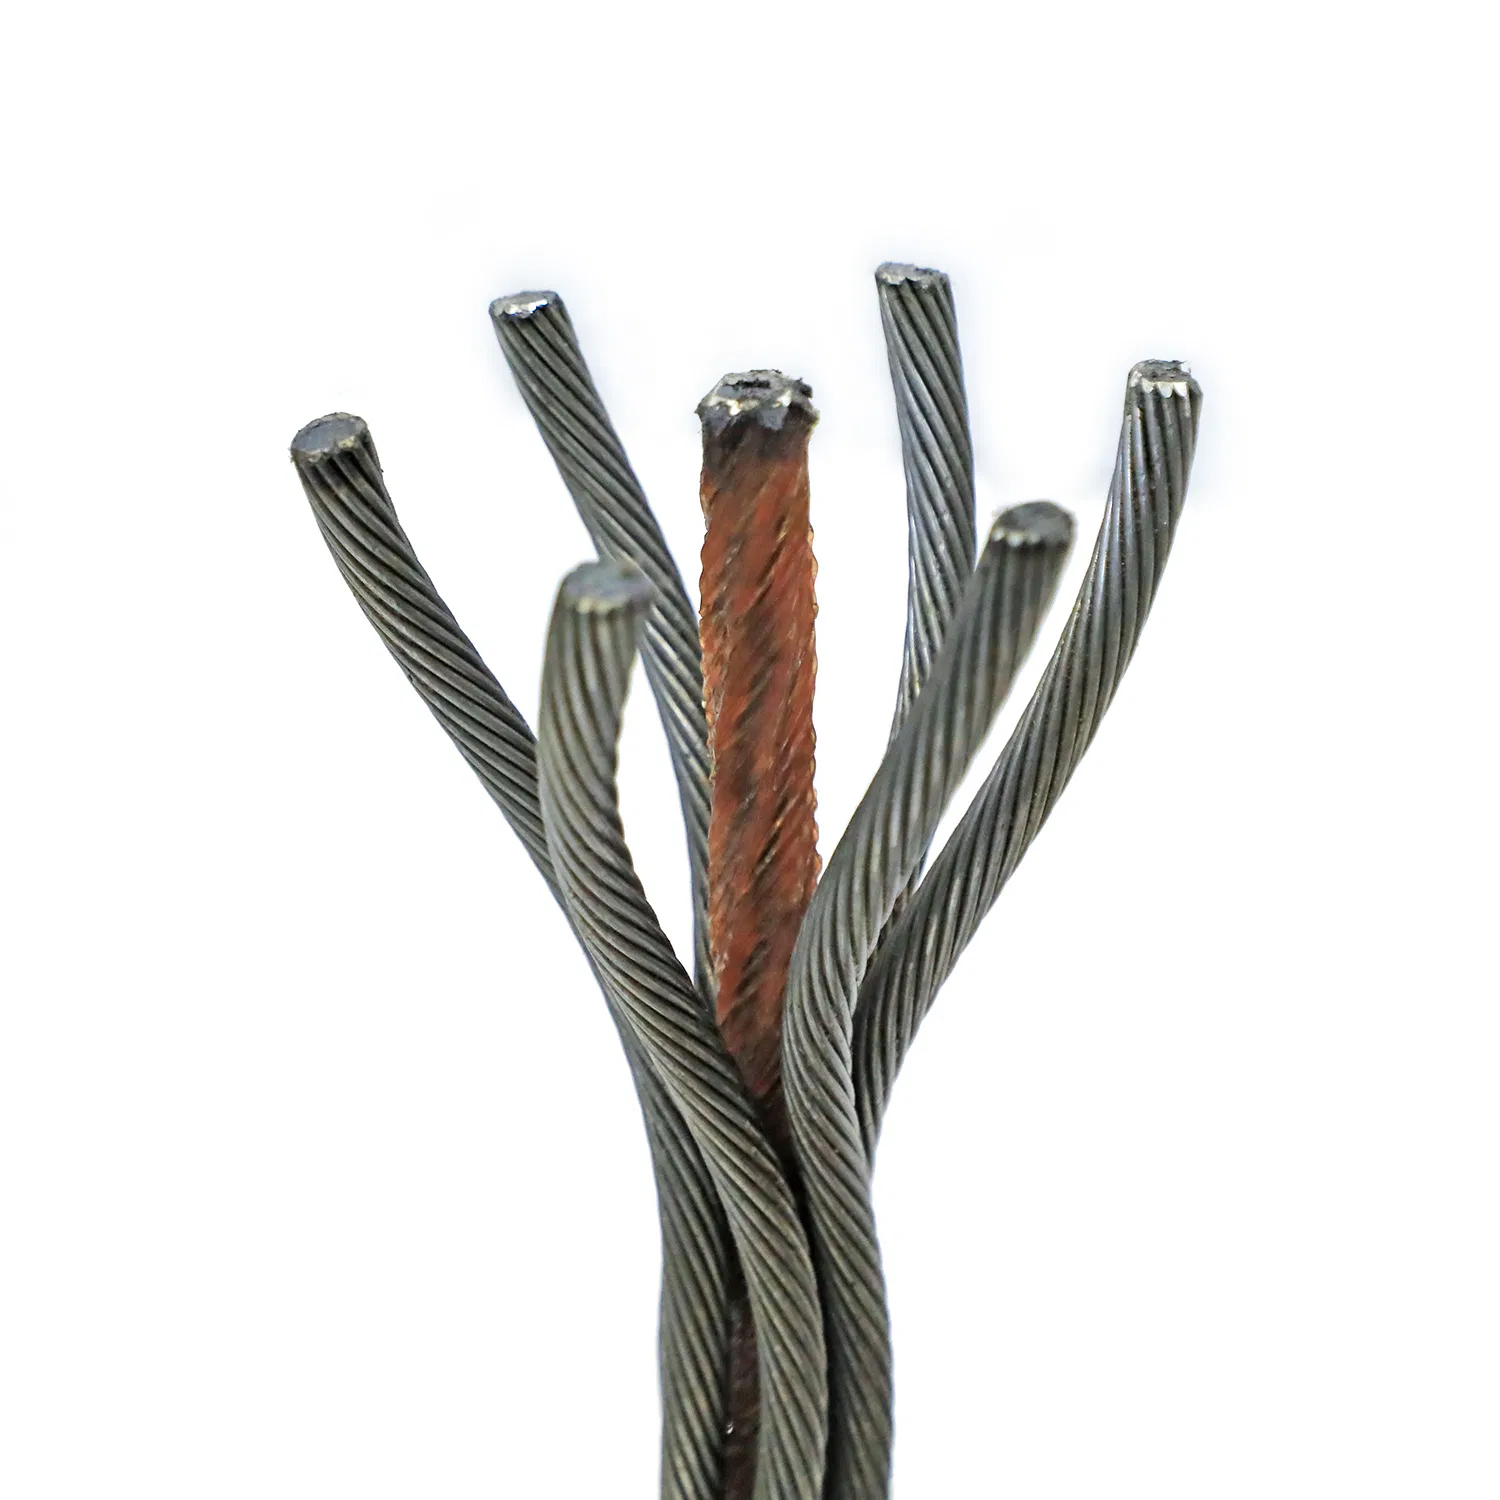
Plastic-coated wire rope has a polymer layer around the outside. Plastic-impregnated rope has polymer within the rope, often between the steel core and outer strands, where it separates moving metal surfaces.
I Look at the Cross-Section
An external coating forms a continuous jacket around the rope. PVC, nylon, polyurethane, and other polymers can protect nearby equipment, improve grip, provide color, and create a barrier against dirt or moisture. The finished outside diameter is larger than the underlying steel rope diameter.
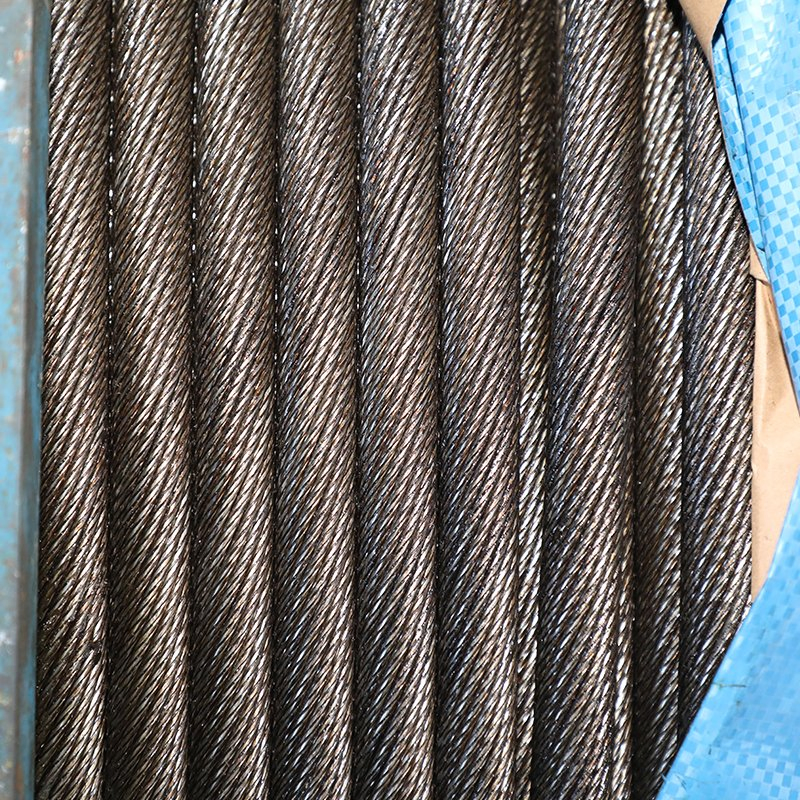
Plastic impregnation places polymer inside the rope structure. The polymer can fill gaps or form a layer around an independent wire rope core. The outer steel strands can remain visible. This design targets internal contact, lubricant retention, and strand support during bending.
| Design | Polymer location | Main purpose | Common limitation |
|---|---|---|---|
| Externally coated rope | Around the outside surface | Surface protection and controlled contact | Steel wires become harder to inspect |
| Plastic-impregnated rope | Inside the rope structure | Internal wear and fatigue control | Selection must match the machine and sheaves |
| Plastic-coated IWRC | Around the steel core | Separate core and outer strands | External wires still need corrosion control |
| Filled-and-coated design | Internal spaces and possibly exterior | Combined project-specific protection | Diameter, heat, and inspection need close control |
I Do Not Treat Polymer as Strength
The steel rope carries the primary tensile load. I do not add the plastic area when I calculate metallic cross-section or breaking force. I use the manufacturer’s declared minimum breaking force for the exact construction and grade.
Polymer can improve service conditions, but it can also change diameter, stiffness, heat behavior, groove contact, and inspection access. I approve the complete rope design rather than asking only for a coating color.
When Should I Choose Plastic-Coated Wire Rope?
I choose an external coating when the rope surface must interact gently with people, products, guides, or the environment.
I use plastic-coated wire rope when I need a smooth outer surface, added environmental separation, color identification, reduced marking, quieter contact, or protection for adjacent parts in a suitable application.
I Match the Benefit to the Application
Fitness equipment, architectural cables, controls, barriers, display systems, and some marine or industrial uses can benefit from an external jacket. The coating can reduce metal-to-metal contact and help keep dirt away from the rope surface.
I still check whether the rope will run over sheaves. A coating can wear, creep, or build heat. A soft polymer may grip a groove differently from steel. A thick jacket can change the effective bending diameter and the fit in drums, guides, ferrules, and end fittings.
I Choose the Polymer, Not Just the Color
PVC is widely used and cost-effective for general protection. Nylon can offer good toughness and abrasion behavior in suitable conditions. Polyurethane can provide strong wear resistance and flexibility. The correct choice depends on temperature, ultraviolet exposure, chemicals, water, hardness, elongation, flame behavior, and required life.
| Service need | Property I review | Why it matters |
|---|---|---|
| Outdoor exposure | UV and weather resistance | Some polymers crack or fade in sunlight |
| Repeated bending | Flexibility and adhesion | A rigid coating can split at the bend |
| Abrasive contact | Wear resistance and hardness | A soft jacket can cut or peel |
| Cold service | Low-temperature flexibility | The coating may become brittle |
| Chemical exposure | Compatibility data | Oils, acids, solvents, or cleaners can attack polymer |
| Food or public contact | Regulatory and surface requirements | General industrial compounds may not be acceptable |
I Plan Inspection Access
An external jacket hides the wires below it. This is a serious tradeoff. A clean-looking coating does not prove that the steel is free from corrosion or broken wires. Damage can begin at a cut, fitting, or small crack and travel under the cover.
I define inspection methods before use. I check coating condition, diameter change, localized swelling, hard spots, discoloration, exposed steel, and termination areas. I use the rope manufacturer’s discard criteria and the equipment rules that apply to the installation.
When Should I Choose Plastic-Impregnated Wire Rope?
I choose impregnation when internal rope movement is a main source of wear or fatigue. This is common in demanding bending and high-cycle systems.
I select plastic-impregnated wire rope when I need the polymer to separate internal steel surfaces, retain lubricant, stabilize strands, reduce internal wear, and support longer fatigue life under suitable operating conditions.
I Control Internal Contact
Outer strands move relative to the core when a rope bends over a sheave. Wires also move inside each strand. This movement produces contact pressure, fretting, and heat. Plastic inside the rope can reduce direct steel-to-steel contact and help distribute pressure.
The polymer can also limit the entry of abrasive particles. It can keep lubricant closer to the working surfaces. These benefits can support cranes, mining machines, hoists, and other high-cycle equipment when the rope and reeving system are correctly matched.
I Match the Construction to the Machine
I never replace a conventional rope with an impregnated rope only because the new rope sounds more advanced. I review drum design, sheave diameter, groove profile, fleet angle, line speed, load spectrum, layer winding, rope rotation, and termination.
A compacted outer strand can improve contact area and crushing resistance. An eight-strand construction can improve bending behavior in some systems. A rotation-resistant construction can control load rotation. Plastic impregnation supports these designs, but it does not replace correct reeving or maintenance.
| Machine factor | Question I ask | Selection effect |
|---|---|---|
| Sheave diameter | Is the D/d ratio suitable? | Small bending ratios raise fatigue demand |
| Groove profile | Does the groove support the rope correctly? | Tight or wide grooves change pressure and wear |
| Drum winding | Is the rope single-layer or multilayer? | Multilayer winding increases crushing and crossover wear |
| Line speed | How much heat can the system create? | Polymer and lubricant must tolerate temperature |
| Load cycle | How often and how heavily does the rope work? | Fatigue resistance becomes more important |
| Rotation | Can the load or rope rotate? | Construction choice may be critical for stability |
I Keep External Inspection in the Plan
Many plastic-impregnated ropes leave the outer strands visible. This helps visual inspection, but internal condition is still not fully visible. I monitor broken wires, diameter reduction, corrosion, waviness, birdcaging, core changes, and unusual stiffness.
I also watch for polymer extrusion. Polymer that appears between strands can indicate pressure, heat, or internal movement. I do not assign a discard decision from one sign alone. I follow the manufacturer and the applicable inspection standard.
How Do Coating, Galvanizing, and Stainless Steel Compare?
I compare the entire corrosion and wear system. Polymer is only one layer of protection.
I use galvanizing to protect exposed steel, stainless steel for suitable high-corrosion applications, external coating for a surface barrier, and impregnation for internal movement control. Some projects combine these features.
I Separate Corrosion Resistance from Wear Control
Galvanizing places zinc on the steel wires. The zinc can protect steel after small surface damage, but it wears over time. Stainless steel resists corrosion through its alloy chemistry, but grade, strength, cost, and galling behavior still matter.
An external polymer jacket creates a barrier while it remains intact. It does not provide the same sacrificial protection as zinc. Internal plastic reduces contact but may not cover exposed outer wires. I often use galvanized wires with plastic impregnation when the project needs both external corrosion resistance and internal wear control.
| Option | Strong point | Tradeoff I review |
|---|---|---|
| Bright steel rope | Strength and cost for controlled environments | Low corrosion protection |
| Galvanized rope | Practical corrosion resistance | Zinc can wear and affect some strength values |
| Stainless steel rope | Strong corrosion performance in suitable grades | Higher cost and different mechanical properties |
| External polymer coating | Surface barrier and contact protection | Hidden steel and coating degradation |
| Internal plastic impregnation | Reduced internal contact and lubricant retention | More specialized machine matching |
I Check Mixed Materials
Water and different metals can create galvanic effects. A stainless rope connected to carbon-steel fittings still needs a system review. Polymer can separate surfaces, but it can also trap moisture at a damaged edge.
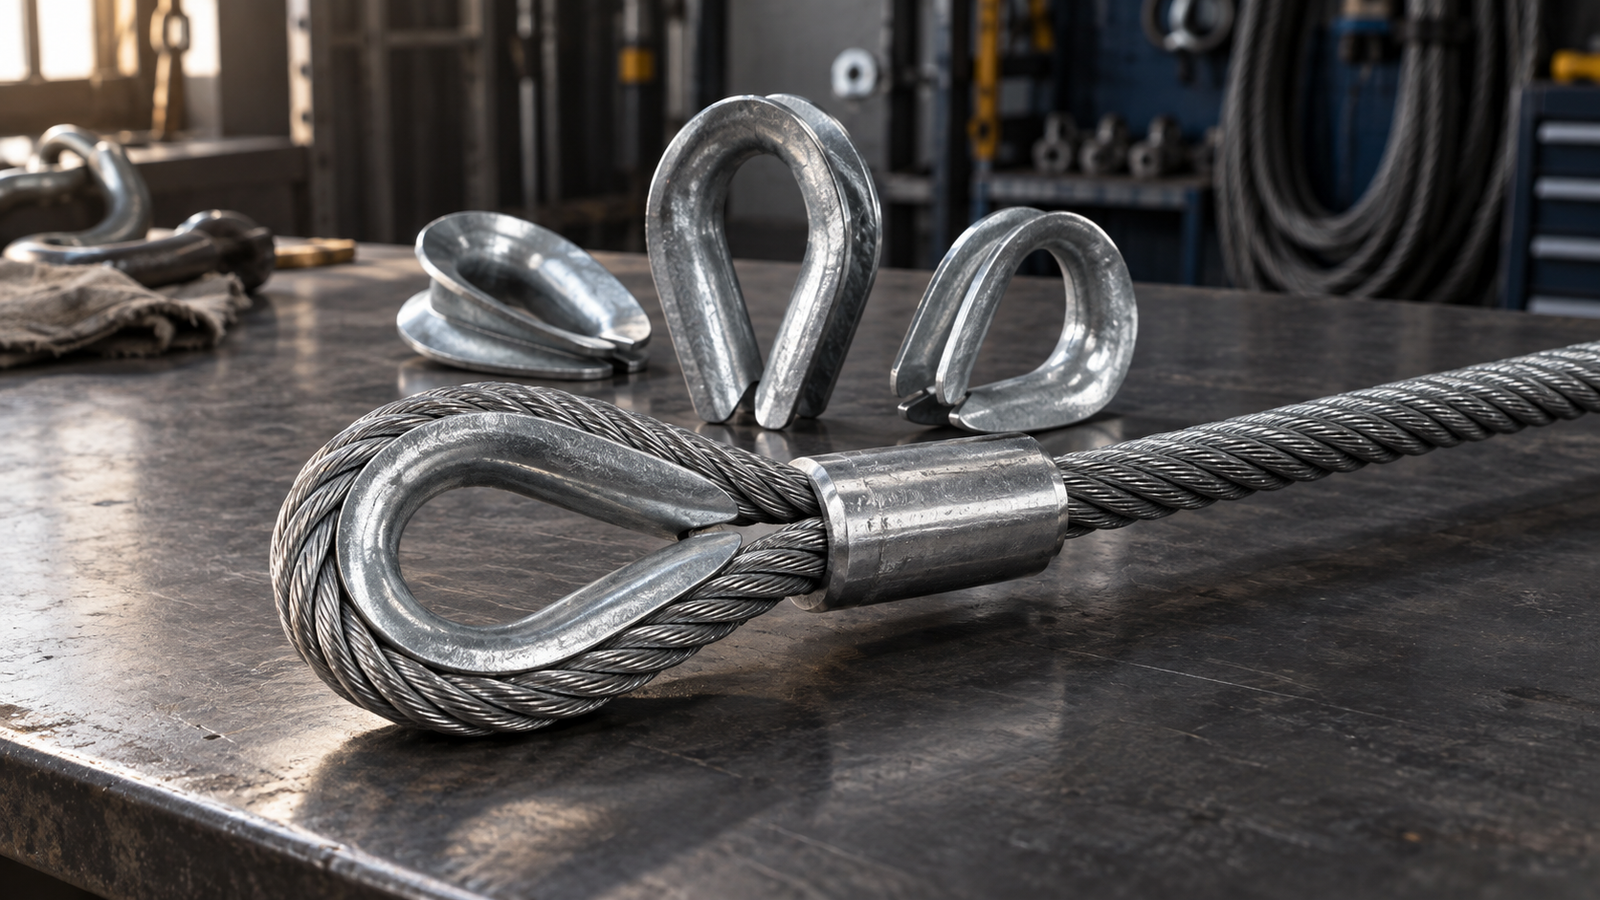
I specify the rope, fittings, sleeves, thimbles, sockets, and structure together. I also confirm whether the termination process removes any coating. A cut coating edge is often the most vulnerable point.
How Do I Specify the Correct Diameter and Strength?
I write both the steel rope diameter and the finished outside diameter when a coating changes the size. One diameter value is often not enough.
I specify the nominal steel diameter, finished coated diameter, construction, core, grade, minimum breaking force, polymer type, thickness, color, tolerance, and compatible fittings as separate purchase requirements.
I Avoid Diameter Confusion
A buyer may request “10 mm coated cable.” This can mean 10 mm steel rope plus coating, or a finished outside diameter of 10 mm. Those products can have different steel areas and breaking forces.
I state values in a clear format, such as “8 mm steel rope, coated to 10 mm outside diameter.” For impregnated rope, I state the nominal rope diameter used for the sheave and strength calculation. I rely on the manufacturer’s data sheet for tolerance and measured diameter method.
I Use Declared Breaking Data
I do not estimate minimum breaking force from finished coated diameter. I use the specified rope construction, grade, metallic area, and manufacturer data. I then apply the equipment or assembly design factor required by the project.
Working load is not a universal fraction printed on every coil. The application, standard, dynamics, angle, termination efficiency, and inspection regime affect the allowed load. A qualified person should approve critical systems.
| Specification field | Example of a clear requirement |
|---|---|
| Steel diameter | 8 mm nominal |
| Finished diameter | 10 mm after coating |
| Construction | 7×19 or project-defined construction |
| Steel finish | Galvanized |
| Polymer | UV-stabilized polyurethane, grade agreed |
| Minimum breaking force | Manufacturer-declared value for the steel rope |
| Color | Black, red, or project code |
| Length and tolerance | 500 m reel, agreed tolerance |
What Quality Checks Should I Request?
I turn general words like “high quality” into measurable inspection points. This keeps the sample, production, and delivered reel consistent.
I request checks for rope diameter, breaking force, coating thickness, concentricity, adhesion, surface defects, polymer properties, length, identification, packaging, and certificates that match the agreed product and application.
I Inspect the Steel Rope First
Polymer cannot correct a poor steel rope. I confirm wire quality, strand construction, lay, core, lubrication, diameter, and minimum breaking force. I also review torsion, bending, or other production controls when they apply to the rope design.
When EN 12385-4 applies to the ordered steel wire rope, I state that scope in the purchase order. I do not assume that the standard automatically covers every coated product, termination, sling, or machine installation.
I Inspect the Polymer System
I check coating thickness around the circumference. I look for bubbles, cracks, thin spots, contamination, poor adhesion, uneven color, and exposed wires. For impregnation, I review polymer distribution and any project-defined sample section.
I ask for polymer data that matters to the environment. This may include hardness, tensile properties, elongation, temperature range, UV resistance, flame performance, or chemical compatibility. I request only the tests that the application actually needs.
I Define Documents Before Production
I can arrange BV, CE, RMRS, DNV, ABS, or other documentation when the buyer defines the exact requirement. A logo on a general certificate is not the same as a witnessed test or product approval.
I ask whether the buyer needs a material certificate, inspection certificate, breaking test, dimensional report, third-party witness, design review, or batch traceability. I confirm the scope before manufacturing because some witness points cannot be added after production.
How Do I Compare Total Cost and Service Life?
I compare cost per operating cycle or cost per ton handled. Purchase price alone can hide downtime, inspection, and replacement costs.
I compare rope price, expected life, installation time, machine wear, inspection access, lubrication, downtime, disposal, and failure risk before I decide whether coating or impregnation gives better value.
I Use Application Evidence
A coated rope can be the best value when it prevents product marking or protects a guide. An impregnated rope can be the better value when internal fatigue controls replacement intervals. A simple galvanized rope can still win when inspection access and low cost matter most.
I begin with a controlled trial when operating history is limited. I record hours, cycles, loads, sheave condition, lubrication, diameter, broken wires, coating damage, and reason for removal. I compare equivalent duty periods, not isolated impressions.
| Cost factor | Question I ask |
|---|---|
| Purchase | What is the delivered and certified price? |
| Installation | Does diameter or stiffness change handling time? |
| Machine wear | Does the surface affect grooves, guides, or drums? |
| Inspection | Can the rope be inspected with available methods? |
| Downtime | How long does a planned or unplanned change take? |
| Service life | What evidence supports the expected improvement? |
| Risk | What happens if the wrong design fails early? |
I Keep Procurement and Engineering Connected
The lowest quote can omit polymer grade, steel diameter, breaking force, or document scope. I do not compare those quotes as equal. I issue one technical specification and ask every supplier to state deviations.
I also ask for a cross-section drawing and a sample when the construction is new. These simple items often reveal whether the seller means an external jacket, a coated core, or full impregnation.
Conclusion
I choose external coating for surface protection and internal impregnation for wear control, then verify diameter, strength, machine fit, inspection, documents, and total operating cost.