The short answer: for freely suspended hammers and vibro hammer suspensions, the default rope is a compacted rotation-resistant 35WXK7 (35 strands, Warrington wires, counter-laid layers, steel core); for leader-guided hammer lines, where the hammer cannot spin the rope, compacted 6×K36WS+IWRC is the workhorse; and every rope on the rig should be sized at a 5:1 design factor against the hammer’s snatch load — not the hammer’s weight — with hot-dip galvanized wire or a plastic-impregnated core wherever mud and water are part of the job. Pile driving is the most violent duty a wire rope will meet on any construction site, and the rope decisions that matter are different from crane work. In this guide I walk through the rope circuits on a piling rig, what the hammer does to the steel, how to choose construction and core, how to size the rope, and when I retire a hammer line.
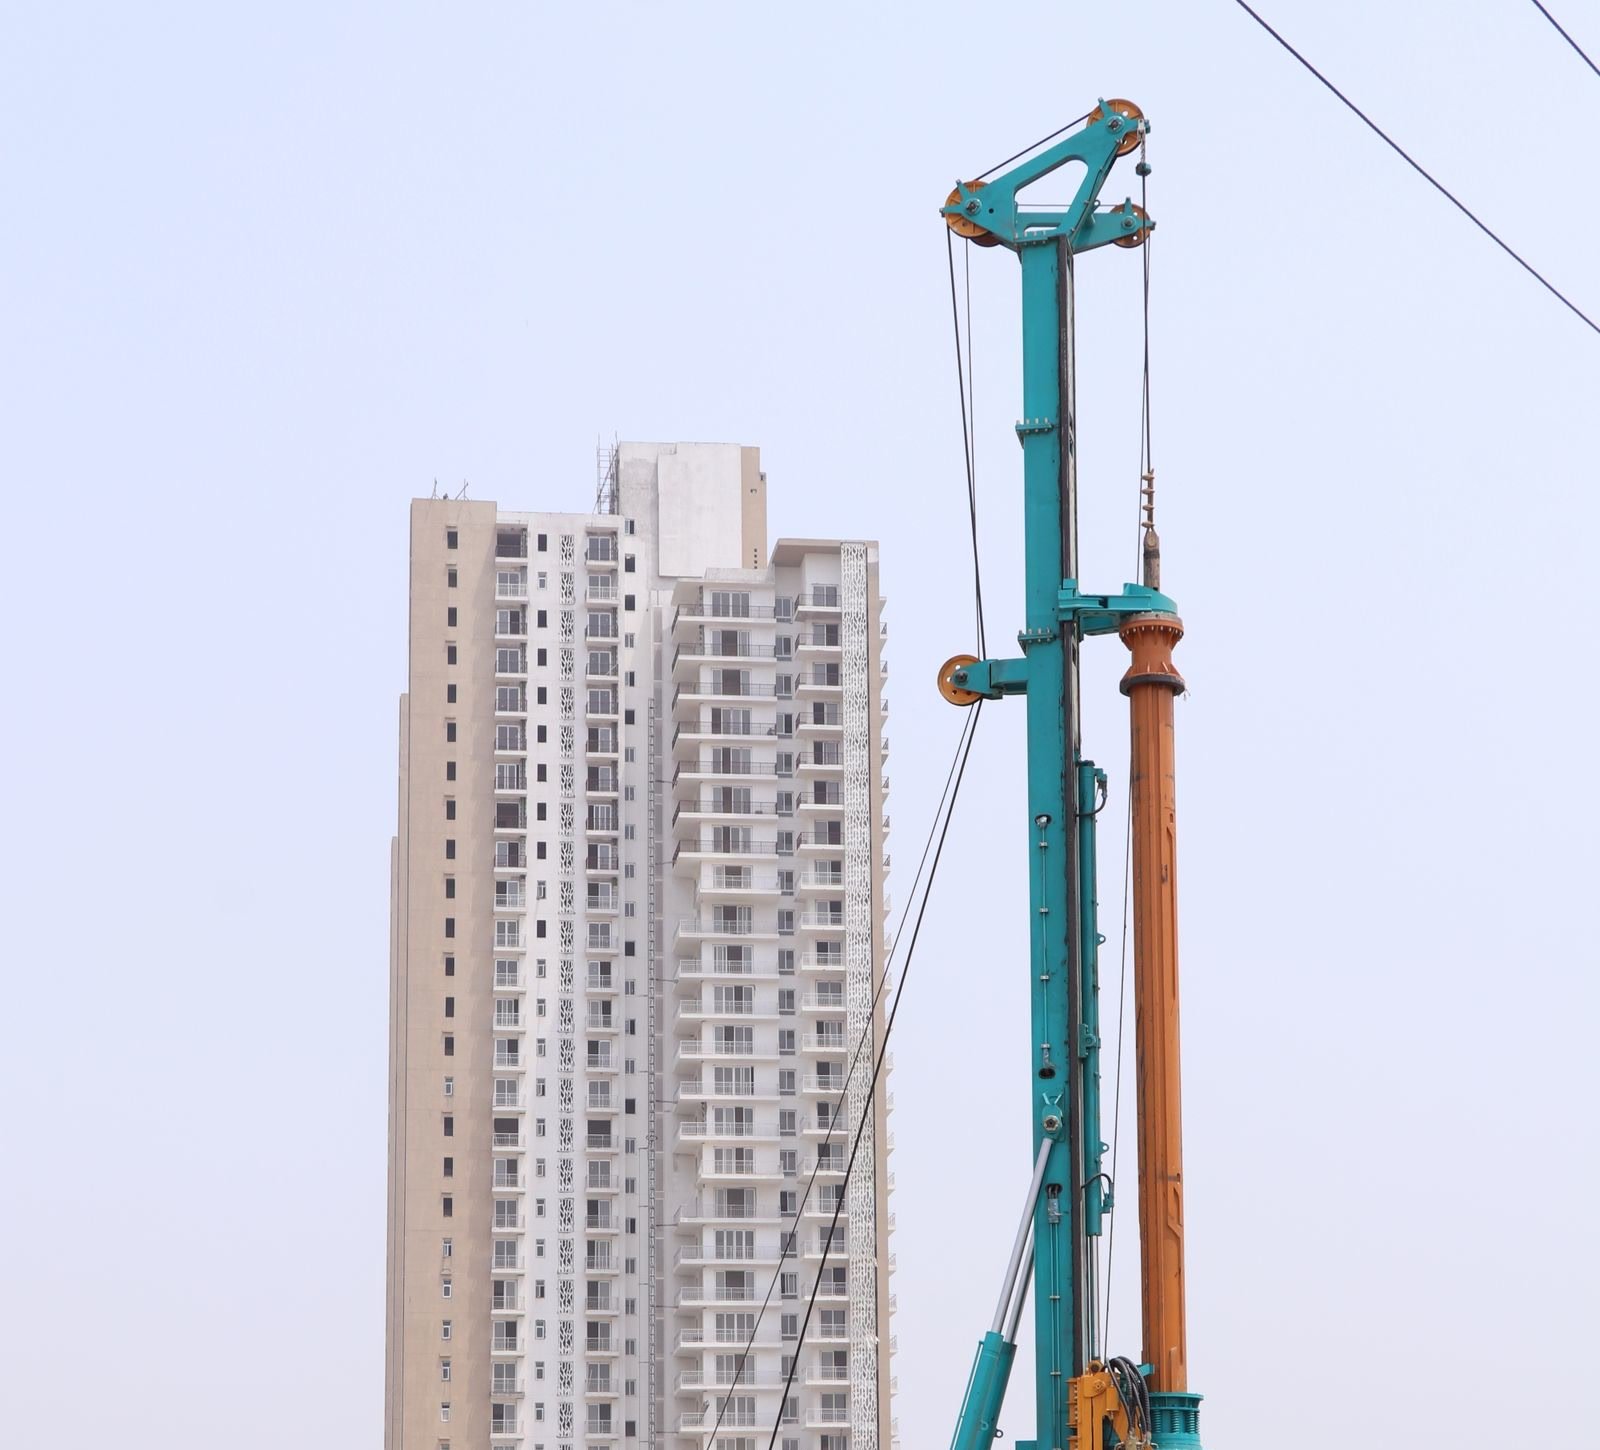
Why Pile Driving Destroys Ropes Faster Than Crane Work
I have supplied ropes to cranes, dredgers and rigs for years, and piling remains the application where customers burn through rope fastest. A crane rope lifts, holds and lowers; a hammer line drops. Four mechanisms are working against it:
- Shock load at every cycle. When the hammer is released and drops onto the pile — or the vibro hangs snatching in its suspension — the dynamic peak can reach roughly twice the static load. Size the line to the hammer’s nameplate weight and you have already lost half the margin.
- Cycle count. A hard-driving piling gang can put several thousand lift-and-drop cycles on a hammer line in a single shift. Bending fatigue over the crown sheaves accumulates at a rate crane ropes never see.
- Abrasion in the leaders and on the drum. The rope rides in leader guides, brushes past the pile and spools in multi-layer wraps where every wrap crushes the one beneath.
- Mud, water and grit. Drilling mud, groundwater and site dust work into the strands and grind the rope from the outside and the inside. Bright (ungalvanized) rope rarely survives this environment.
There is also a piling-specific torsion problem: a freely suspended hammer or vibro hanging on a crane hook can rotate, and an ordinary 6-strand rope under load will happily spin and birdcage. That is the single most important fork in the selection road, and it comes next.
The Rope Circuits on a Piling Rig
“Piling rope” is not one rope. Depending on the machine, you may be buying two to four different circuits, and each punishes the steel differently:
| Machine / circuit | What it does | Main duty | Typical construction |
|---|---|---|---|
| Leader rig hammer line (diesel or hydraulic hammer on leaders) | Winch → crown sheave → hammer; lifts the hammer, sometimes the whole ram | Thousands of shock cycles per shift, abrasion in leader guides, multi-layer drum | Compacted 6×K36WS+IWRC, grade 1960–2160 (rope cannot rotate — the hammer is guided) |
| Crane-suspended hammer / vibro suspension | Hangs hammer, vibro or hydraulic press from the crane hook via slings | Free hanging — load can spin; snatch at drop; long unsupported lengths | Rotation-resistant 35WXK7 or 35×K7, IWRC or EPIWRC core |
| Main hoist (pile, casing, auger handling) | Handles sheet piles, casings, reinforcement cages and hanging leads | Heavy lifts, single-part or multi-part reeving, rotation risk on single-fall | 35WXK7 (single fall) or 35×K7; 6×K36WS+IWRC where guided |
| Guide-located drop hammer rope | Winch-operated drop hammer running in the leaders | Severe impact, slow speeds, small sheaves | Compacted 6×K36WS+IWRC or 6×36WS+IWRC |
| Auxiliary / spot lines | Spotting, wedging and light handling | Frequent bending over small sheaves, lower loads | Flexible 6×36WS+IWRC |
In this article I focus on the hammer line and the suspension ropes, because they are the ones that fail expensively — a parted hammer line drops several tonnes of steel onto the pile, the helmet and everything below it.
Choosing the Construction
Rotation-resistant or not? The first decision
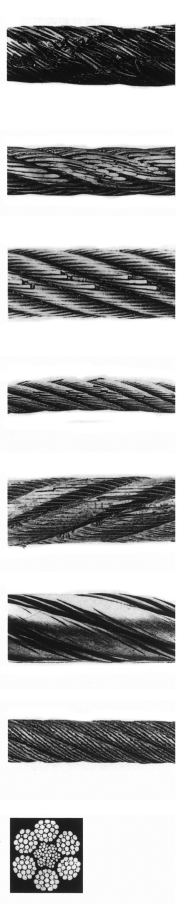
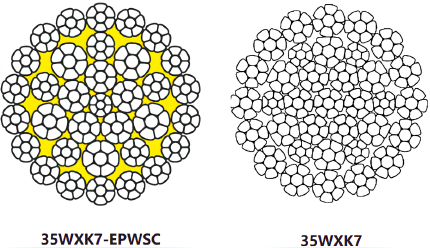
Ask one question before anything else: can the load spin? If the hammer or vibro hangs free on a crane hook, the answer is yes — and an ordinary 6-strand rope will unlay itself, lose lay length and eventually birdcage. That duty needs a rotation-resistant rope: 35WXK7 (my default) or 35×K7, whose strand layers are laid in opposite directions so the torques cancel under load. The same logic applies to single-fall main hoisting of pile and casing — see my tower crane rope guide for the physics in detail.
If the hammer runs in the leaders, it is guided and cannot spin the rope — and here I actually prefer a conventional 6-strand rope, because rotation-resistant ropes are more sensitive to crushing and shock than a well-built compacted 6-strand. Compacted 6×K36WS+IWRC is the hammer-line standard: dense, tough, and forgiving of the multi-layer drum.
Why compacted strands earn their premium here
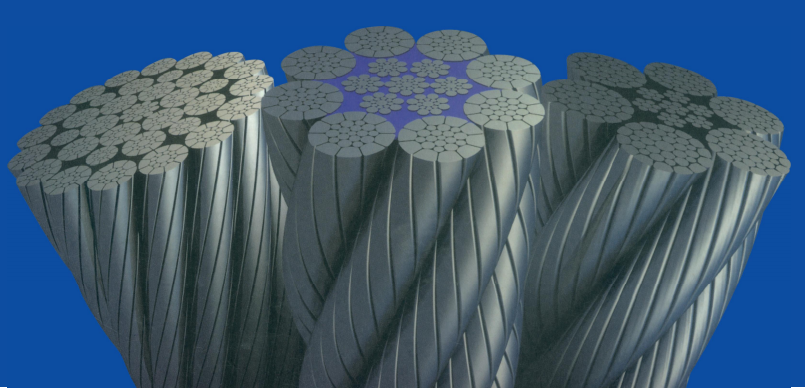
Compacting (the “K” in EN 12385 naming) presses the strands after stranding, raising the metal fill factor by roughly 10–15%. For piling this pays twice: the breaking force goes up without changing the drum and sheave package, and the smooth, dense outer surface resists the abrasion of leader guides and drum crossovers far better than a round-strand rope. When a hammer line dies of wear at 60–70% of its expected life, the rope was almost never compacted.
Core: IWRC, and consider EPIWRC
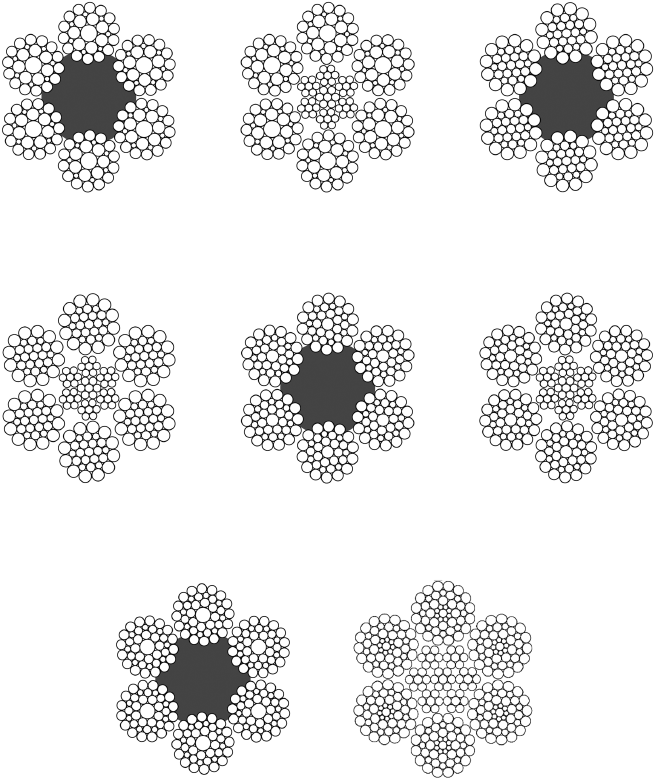
Steel core (IWRC) is mandatory on hammer lines and hoists — a fiber core crushes between drum layers and gives up strength exactly where piling needs it. On leader rigs working in mud and water I push customers one step further to EPIWRC (plastic-impregnated core): the polymer layer locks the factory lubricant into the core, cushions the strands against inter-strand wear and seals groundwater out of the rope’s heart. On ropes that died of internal corrosion, EPIWRC is usually the cheapest fix available.
Finish: galvanized, always
Piling sites are mud, rain and groundwater by definition. Hot-dip galvanized wire is the default for every rope on a piling rig; the zinc sacrifices itself before the steel corrodes. Bright rope is defensible only for short-duration, dry indoor work — and even then I check the rope log more often. Combined with an EPIWRC core, galvanized construction routinely doubles corrosion-driven rope life on wet sites.
| Construction | Strengths | Watch out for | Best for |
|---|---|---|---|
| 35WXK7 (rotation-resistant, compacted) | Neutral torque, high MBL, crush-resistant multi-layer spooling | Stiffer, more shock-sensitive than 6-strand, needs correct break-in | Freely suspended hammers, vibro suspensions, single-fall main hoist (my default) |
| Compacted 6×K36WS+IWRC | +10–15% MBL, dense abrasion-resistant surface, tough under shock | Not rotation-resistant — guided duty only | Leader-guided hammer lines, drop hammers, guided auger hoists |
| 6×36WS+IWRC | Flexible, good fatigue life, economical | Lower MBL per diameter than compacted | Auxiliary and spot lines, light drop-hammer duty |
| 35×K7 (rotation-resistant) | Excellent rotation resistance, flexible | More shear-sensitive; strict discard limits | Smaller rigs, lighter suspended loads |
| Any of the above with EPIWRC core | Sealed, lubricated core; better fatigue; corrosion barrier | Slightly larger outside diameter; cost premium | Muddy, wet leader rigs; anything dying of internal corrosion |
Sizing the Rope: Design Factor Against the Snatch, Not the Weight
For hammer lines and suspensions I size to a 5:1 design factor against the dynamic peak load, and I do not go below 4:1 under any circumstances. Estimate the dynamic peak as the hammer’s static load multiplied by a snatch factor of roughly 1.8–2 for impact hammers and hard-release vibro work:
Worked example: hammer plus helmet and cap weigh 9 t static. With a snatch factor of 2, the peak line load is about 18 t ≈ 177 kN. Required MBL ≥ 5 × 177 kN ≈ 883 kN. A 32 mm compacted 6×K36WS+IWRC at 1960 N/mm² delivers roughly 800 kN — not enough. Step up to 34 mm (≈904 kN) and the margin absorbs years of leader wear, mud and shock. The same breaking-force arithmetic I use for cranes is in my breaking strength and safety factor guide.
| Diameter | MBL, compacted 6×K36WS+IWRC, 1960 N/mm² (approx.) | Max hammer peak load at 5:1 design factor |
|---|---|---|
| 26 mm | ≈529 kN (≈53.9 t) | ≈106 kN (≈10.8 t) |
| 28 mm | ≈613 kN (≈62.5 t) | ≈123 kN (≈12.5 t) |
| 32 mm | ≈800 kN (≈81.6 t) | ≈160 kN (≈16.3 t) |
| 34 mm | ≈904 kN (≈92.2 t) | ≈181 kN (≈18.4 t) |
| 36 mm | ≈1013 kN (≈103.3 t) | ≈203 kN (≈20.7 t) |
| 40 mm | ≈1251 kN (≈127.6 t) | ≈250 kN (≈25.5 t) |
Nominal minimum breaking forces estimated by the EN 12385-4 method for this class (compacted values ≈12% above standard 6×36WS+IWRC); always confirm against the manufacturer’s breaking-force certificate for the delivered lot. And check the drum before upsizing: the extra diameter costs spooling capacity fast, and a hammer line that overfills the drum will crush itself to death before its time.
Installation and Break-In: Where Good Ropes Are Ruined
A premium hammer line can be wrecked in its first hour. The rules I insist on:
- Unreel, never uncoil. A dropped coil kinks permanently — and a kinked rope is scrap, no exceptions.
- Seize both sides of every cut so the construction cannot open while you work.
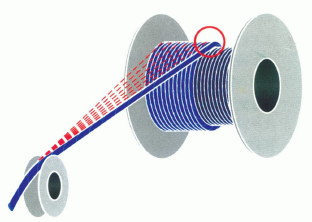
- Spool under back tension (2–5% of breaking force) with the fleet angle kept near 1.5°, matching lay direction to the drum so the rope winds without crossovers. Full routine in my installation and maintenance guide.
- No swivel on rotation-resistant rope. A swivel under a 35WXK7 lets the counter-laid layers unlay themselves — it defeats the design. Let the rope’s structure do the anti-rotation work.
- Break it in gently: the first shifts at reduced hammer drop height and moderate loads, so strands and core bed into each other before the first full-energy driving.
- Match the sheaves: worn or undersized crown sheaves and leader rollers shave years off the rope. Groove diameters should run 5–10% over nominal rope diameter.
Inspection: Retiring a Hammer Line Before It Retires Itself
I inspect piling ropes against ISO 4309, weighted toward the damage zones piling creates. The hammer line’s hot spot is predictable: the section that rides the crown sheave and leader rollers at the top of the stroke, where every cycle bends the rope. Check it daily, the full length weekly.
| What to check | Discard / action |
|---|---|
| Broken wires in the working zone (6-strand) | Retire at about 6 broken wires in one lay length or 10 in 30 rope diameters |
| Broken wires (rotation-resistant 35WXK7 / 35×K7) | Far stricter: retire at 2 breaks in 6 rope diameters or 4 in 30 — assess at the first valley breaks too |
| Diameter reduction | Retire at ~7% diameter loss (IWRC rope); measure with calipers at several points, flattening counts |
| Wear flats from leader guides | Crown wear approaching half the wire diameter: end-for-end the rope now, or retire |
| Corrosion | Deep pitting or rust bleeding between strands = internal attack; retire even if the wire count passes |
| Kinks, birdcaging, shock loops | Retire immediately — typically from slack rope pulled tight or a dropped hammer snatching the line |
| Terminations | Inspect sockets, wedge sockets and splices at every shift for pulled wires, movement and corrosion |
Keep a rope log with cycle counts and inspection dates — the crews with the best records replace ropes on evidence, not luck, and they replace fewer of them. The general criteria are the same I apply to cranes and crawlers, and the machine-side view is in my crawler crane wire rope guide.
Lubrication: The Cheapest Rope Life on Site
A wire rope is a machine of hundreds of wires sliding over one another, and the hammer’s shock loads squeeze the factory lubricant out of the strands early. Clean the rope, then apply a penetrating rope lubricant that reaches the core — on hard-driving gangs that means every 40–80 operating hours. Skip engine oil and general-purpose sprays: they never reach the core and they wash off in the first rain. Well-lubricated hammer lines routinely outlast dry ones two to one on the wet sites I follow.
Final Word: Buy for Shock and Rotation, Not Just Diameter
Every premature piling rope failure I have investigated traces back to one of five decisions: sizing to the hammer’s weight instead of the snatch, ordinary 6-strand under a freely suspended hammer, a fiber core, bright wire on a wet site, or a skip-a-week lubrication habit. Fix those five, add the 5:1 rule and a honest break-in, and the hammer line will give you everything it has. Sister applications use related logic — see my rotary drilling rig 35WXK7 guide and my article on why wire ropes fail.
Aulone is a professional manufacturer and supplier of steel wire ropes, wire rope slings, synthetic ropes and rigging hardware for lifting, marine, mining, construction and industrial applications. With more than 20 years in the industry, 200,000 tons of annual capacity and production to EN 12385-4 under ISO 9001 — certified by BV, ABS, DNV, RMRS and CE — we supply compacted, galvanized and plastic-impregnated hammer lines and rotation-resistant ropes with lot-specific breaking-force certificates, keep common piling sizes in stock, build custom assemblies with pressed or spliced terminations, and arrange third-party testing on request. For help speccing your next hammer line, write to me at info@wireropes.net.
Frequently Asked Questions
What is the best wire rope for pile driving?
For leader-guided hammers: compacted 6×K36WS+IWRC, hot-dip galvanized, grade 1960 or higher. For freely suspended hammers, vibro suspensions and single-fall hoisting: compacted rotation-resistant 35WXK7 with IWRC or EPIWRC core. Size either at 5:1 against the dynamic peak load, and confirm the MBL on the lot certificate.
Should a hammer line be rotation-resistant?
Only if the load can spin. A hammer running in the leaders is guided and cannot rotate the rope, so a compacted 6-strand is actually the tougher choice there. A hammer or vibro hanging free from a crane hook can spin the rope, and an ordinary 6-strand will unlay and birdcage — that duty needs 35WXK7 or 35×K7.
Why do hammer lines fail so much faster than crane ropes?
Shock load and cycle count. Every hammer release spikes the line tension to roughly twice the static load, and a productive gang repeats that several thousand times per shift. Fatigue and wear accumulate at a rate crane hoist ropes never approach — which is why piling ropes need compacted constructions, honest design factors and disciplined lubrication.
What safety factor should I use for piling wire rope?
I size hammer lines and suspensions at 5:1 minimum breaking force to the estimated dynamic peak (static load × a 1.8–2 snatch factor), and never accept below 4:1. Sizing to the hammer’s nameplate weight alone quietly discards half the margin the rope actually needs.
How often should a pile driving hammer line be lubricated?
Clean and re-lubricate every 40–80 operating hours on hard driving, with a penetrating lubricant that reaches the core. Shock cycling drives the factory grease out of the strands early, and a dry rope corrodes and fatigues from the inside long before surface wear shows.
When should a piling rope be replaced?
Apply ISO 4309: about 6 broken wires per lay length (10 in 30 diameters) for 6-strand rope, 2 in 6 diameters (4 in 30) for rotation-resistant ropes, ~7% diameter loss, any deep corrosion pitting, any kink or birdcage, or a failing termination — and inspect the crown-sheave zone daily because that is where a hammer line dies first.