How to Choose a Wire Rope Manufacturer in China: A Buyer’s Field Checklist
By Andri — Technical Writer & Crane Rope Specialist, Aulone (www.wireropes.net)
The short answer: a good wire rope manufacturer in China proves itself with evidence, not catalogues — an actual factory with its own stranding and closing lines, ropes produced to EN 12385-4 and certified under ISO 9001, batch traceability from wire rod to finished reel, breaking-force test reports that match your shipment, and third-party verification where your application demands it. The country has an enormous, genuinely competitive rope supply base, and for the same specification you can meet anything from world-class mills to resellers repacking commodity rope. I have sat on both sides of this table for over 20 years, and in this guide I’ll give you the exact checklist I would use as a buyer: six steps, a red-flag list, and the documents to demand before a purchase order.
Why the Factory — Not the Price List — Decides the Outcome
Wire rope is a safety component. A rope that arrives 0.3 mm under diameter, or with a breaking force printed on a certificate that was never run, doesn’t fail a paperwork review — it fails over a crane hook, a mine shaft or a ship’s deck. That is why I tell every buyer the same thing: the unit price is the least interesting number on the quotation. What matters is whether the person quoting you controls the steel chemistry, the wire drawing, the stranding, the closing and the testing — or is just forwarding your enquiry to someone who does. Every step below is really the same question asked from a different angle: who is accountable for this rope, and can they show me proof?
Step 1: Confirm You Are Dealing With a Real Manufacturer
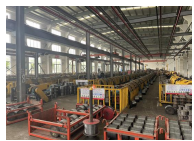
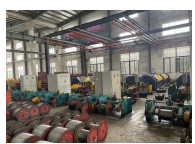
The market is full of trading companies that present themselves as factories, and some of them are perfectly honest intermediaries. But you deserve to know which one you’re talking to, because a trader cannot answer process questions, cannot hold certifications in its own name, and disappears exactly when a quality claim needs engineering answers. The reliable signals: a street address you can verify (not a registered agent in an office tower); the ability to invite you, or a third-party inspector, into a production hall with stranding and rope-closing machines; an in-house laboratory with tensile and fatigue testing equipment; and staff who answer technical questions about lay, preforming and core types without needing to “check with the factory”. Ask for heat numbers and batch records from a recent comparable order. A genuine mill produces traceability documents as a matter of routine; a reseller has to go and ask someone else for them.
Step 2: Test the Construction Range and Technical Depth
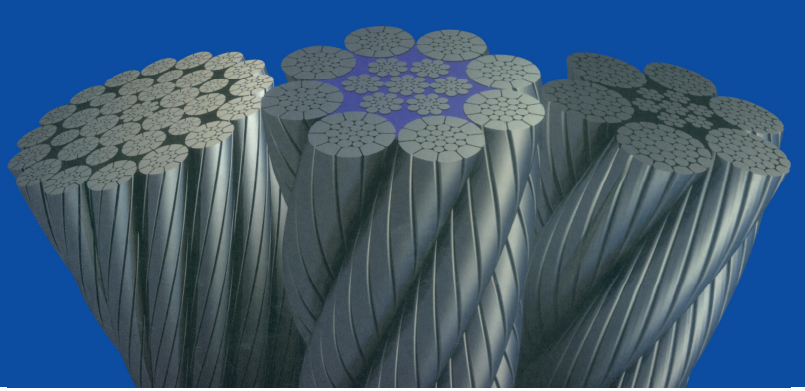
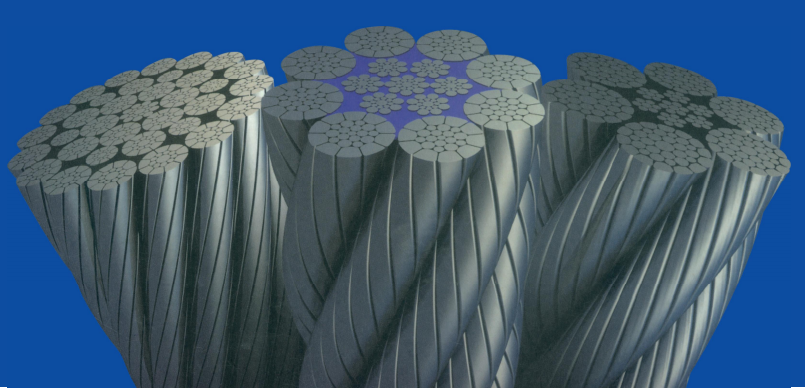
Anyone can list “6×36” on a price sheet. The question is whether the manufacturer can make — and explain — the constructions your equipment actually needs, because cranes, rigs, mines and ports each impose different demands on a rope. Put your working load, design factor, drum and sheave diameters, line speed, duty cycle and environment in front of the supplier and see what comes back. A real manufacturer asks follow-up questions and recommends a documented construction; a middleman quotes whatever is on the enquiry form. This conversation is also where you learn whether they can supply the specialty constructions that separate a mill from a stockist:
| Application | Constructions a capable manufacturer should offer | What it proves |
|---|---|---|
| Mobile & tower cranes | 6×36WS+IWRC, 35×K7 / 35WXK7 rotation-resistant, 18×K7 | Compacted and multi-strand rotation-resistant know-how, not just commodity rope |
| Rotary drilling rigs | 35WXK7 (6×K36WS-EPIWRC), 8×K26WS-EPIWRC for heavy rigs | Compacted, plastic-impregnated IWRC production — an advanced process few mills master |
| Ports (STS cranes) | 4V×39S+5FC, AL FLEX-7 type flat-strand traction ropes | Specialty port constructions and the fatigue data behind them |
| Mining & electric shovels | 6×36WS+IWRC flattened-strand, large-diameter dragline ropes | Big closing machines and experience with 60 mm+ diameters |
| Elevators | 8×19S+FC, 9×21+FC to EN 12385-5 | Smooth-running, tight-tolerance rope for traction duties |
| General & marine | 6×19 / 6×36 series, galvanized and bright, FC / IWRC / WSC cores | Breadth of diameters, finishes and cores from stock |
If you want to go deeper on how construction geometry drives rope behaviour, my 6×36 wire rope specifications guide and the FC / IWRC / WSC core comparison cover the details. And when a supplier talks you through why a compacted rope suits your drum, or why an IWRC beats a fibre core in your environment — instead of just reciting a part number — you have probably found a factory worth shortlisting.
Step 3: Verify Standards and Certifications — Scope and Dates Included
Certificates are where careless buyers get burned, because a scanned PDF proves very little on its own. Certificates have holders, scopes and expiry dates, and the scope is the whole game: a CE certificate for EN 12385-1 (general requirements) is not the same as production compliance with EN 12385-4, the product standard for stranded ropes for general lifting applications. Ask for the current certificate, check that the certificate holder is the entity you are contracting with, and confirm your construction and diameter range fall inside the scope. For marine and offshore work, class society approvals — BV, ABS, DNV, RMRS — are the practical benchmark, because those bodies audit the mill and witness tests themselves. The table below is the checklist I keep:
| What to ask for | Why it matters | Red flag if… |
|---|---|---|
| EN 12385-4 production compliance | The governing product standard for lifting ropes in most export markets | Only “EN 12385-1” or a vague “ISO standard” is offered |
| ISO 9001 quality management certificate | Audited processes, document control and corrective-action systems | Certificate expired, or held by a different company name |
| CE marking with EN 12385 documentation | Required for ropes entering the EU market | “CE” stamped on rope but no supporting technical file |
| Class approvals: BV, ABS, DNV, RMRS | Independent audit and witnessed testing for marine/offshore use | Approvals claimed but certificate numbers cannot be verified |
| Third-party test reports (SGS, TÜV, BV, etc.) | Independent verification of breaking force, fatigue, dimensions | Only in-house reports offered, and only on request — never proactively |
Step 4: Walk the Quality Chain From Wire Rod to Finished Reel
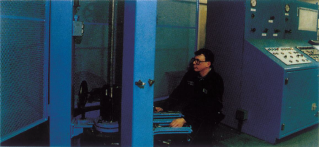
Rope quality is decided long before closing, so ask the manufacturer to describe their process control in sequence. The answer I expect from a well-run mill sounds like this: incoming inspection of wire rod (chemical composition and mechanical properties per heat, with mill certificates retained); drawn wire checked for tensile strength, torsion and ductility at the drawing block; galvanizing or zinc-coating thickness verified where corrosion protection is part of the specification — the finish decision matters more than most buyers realise, as I explain in my galvanized vs bright vs stainless guide; strand and rope diameter, lay length and preforming checked during stranding and closing; and finished-rope testing — breaking force, and fatigue testing for critical constructions — before release.
Then insist on the documents that travel with the order: a certificate of conformity to EN 12385-4, actual measured breaking-force results per production lot (not a data-sheet photocopy), diameter and lay-length measurements, and batch traceability back to the wire heats. For a first order with a new supplier, one more step is cheap insurance: order a sample and send it to an independent laboratory for breaking force and dimensional checks, and compare the results against the declared specification. Ten metres of rope and a few hundred dollars of testing will tell you more than a month of email. Any manufacturer who hesitates at that request is telling you something.
Step 5: Capacity, Stock and Lead Time — Check the Numbers
A supplier can hold every certificate in the industry and still sink your project schedule if they can’t produce. Ask directly for annual production capacity, current utilisation and the maximum single-rope length their closing machines can handle in your diameter. For common crane and general-purpose constructions, ask what is held in stock — a mill that stocks standard 6×36WS, rotation-resistant and galvanized ropes can ship replacement lengths in days, which matters enormously when a rope fails and the crane is standing still. For made-to-order ropes, get a realistic lead time and ask what happens if your order has to be split across deliveries. Export experience is part of capacity too: reels sized to your unspooling equipment, seaworthy packing, correct HS codes and shipping documents, and a named export contact who answers questions in your working hours.
Step 6: Custom Assemblies, Documentation and After-Sales Support
The best manufacturers sell rope systems, not coils. If your equipment needs it, ask whether they supply cut-to-length assemblies re-reeled onto your drum dimensions, with terminations fitted — sockets swaged or spelter-poured, wedge sockets assembled, thimbles and swaged fittings installed — and proof-load documents for the completed assembly. Ask how they handle nonconformance: a serious supplier has a written claims procedure, investigates with engineering involvement rather than a discount offer, and will discuss potential risks honestly even when it makes the sale harder. That honesty, in my experience, is the single most predictive trait of a manufacturer worth a long-term contract — the ones who promise everything in the first email are the ones who go quiet when a rope arrives short or a test report doesn’t match the order.
Red Flags: When to Walk Away
| Red flag | What it usually means |
|---|---|
| Price dramatically below every other quote | Thin gauge wire, missing compaction or coating, or recycled stock — the cost shows up as early rope failure |
| Cannot provide heat numbers or batch traceability | No real mill records — likely a reseller or mixed-stock supplier |
| Certificates without a scope, holder or expiry date | Decorative paperwork, not audited compliance |
| Refuses a factory visit, live video audit or third-party inspection | There is no factory — or there is something to hide |
| Generic test reports with no lot numbers | The report was never run on your rope |
| Dodges technical questions or quotes without asking about your application | An order-taker, not an engineer — expect no support after the invoice |
The Bottom Line From a Rope Specialist
Sourcing wire rope from China rewards buyers who verify and punishes buyers who assume. Check that the supplier owns a factory; probe the construction range with real application questions; verify certificates down to scope and expiry; walk the quality chain from wire rod to breaking-force test; confirm capacity, stock and export logistics; and insist on documentation and honest after-sales handling. Do that, and China’s supply base offers some of the best value in the rope industry — certified, traceable rope at production-economy prices. Aulone is a professional manufacturer and supplier of steel wire ropes, wire rope slings, synthetic ropes and rigging hardware for lifting, marine, mining, construction and industrial applications. With more than 20 years in the industry, an annual capacity of 200,000 tons, ropes produced to EN 12385-4 under an ISO 9001 quality management system, class certifications including BV, ABS, DNV and RMRS with CE marking, we supply certified ropes from stock or as custom assemblies, with third-party testing and complete batch documentation on every order. Send your specification, application details and required lengths to info@wireropes.net and I’ll put together a documented offer — the same checklist applied to ourselves, gladly.
FAQ: Choosing a Wire Rope Manufacturer in China
How can I verify that a Chinese wire rope supplier is a real factory?
Check the registered business scope and street address, then ask for proof of production: a live video walkthrough of the stranding and closing floor, a third-party or in-person audit, heat-number traceability from a recent order, and photos of their own testing laboratory. A genuine manufacturer answers process questions about lay length, preforming and core design directly; a trader needs to forward them and comes back with generic answers.
Which certifications should I ask a wire rope manufacturer for?
Start with the standard your market requires: EN 12385-4 production compliance for lifting ropes sold into Europe, ISO 9001 for the quality system, and CE marking with its supporting technical file. For marine and offshore work, look for class society approvals such as BV, ABS, DNV or RMRS. Always check the certificate holder matches your contracting party, and confirm the scope covers your rope construction and diameter range before the expiry date.
What documents should come with a wire rope order?
At minimum: a certificate of conformity to EN 12385-4, actual breaking-force test results for your production lot (not a catalogue photocopy), measured diameter and lay-length records, batch traceability to the wire heats, and for marine orders the relevant class-society certificate. For critical applications, add third-party inspection or witness testing before shipment.
Should I test samples before placing a bulk order?
Yes, especially with a new supplier or for safety-critical applications. Request a sample from a comparable production run and send it to an independent laboratory for breaking force and dimensional verification against the declared specification. It costs little, takes days, and instantly exposes under-strength wire, wrong cores or overstated certificates. A manufacturer who resists sample testing is a manufacturer to avoid.
Can I order custom rope lengths and terminated assemblies from a Chinese manufacturer?
A capable one, yes. Ask for cut-to-length ropes re-reeled onto your specified drum, with swaged or spelter sockets, wedge sockets or swaged fittings fitted at the factory and proof-load documents for the finished assembly. Confirm the maximum single-rope length their closing machines can produce in your diameter, and agree packing and reel dimensions that match your unspooling equipment before the order is confirmed.
Why is the cheapest quotation usually the most expensive rope?
Rope cost is not the invoice — it is the cost of downtime, replacement labour and risk multiplied over the rope’s life. Thin-gauge wire, skipped compaction, thin galvanizing or an unverified breaking force can halve service life and put the certificate’s MBL in doubt precisely when an inspector asks for it. Compare suppliers on total delivered cost with documented quality: certified rope at a fair price outlasts cheap rope several times over.