Wire Rope Terminations and Fittings: The Complete Guide to Sockets, Clips, Thimbles and Shackles
By Andri — Technical Writer & Crane Rope Specialist, Aulone (www.wireropes.net)
The short answer: a wire rope is only as strong as the fitting on its end. A correctly installed spelter or swaged socket keeps 100% of the rope’s minimum breaking load, a swaged-sleeve Flemish eye keeps around 90–95%, while wire rope clips and wedge sockets — the common field options — hold only about 80%, and considerably less if fitted carelessly. Choosing the right termination, installing it exactly to the manufacturer’s procedure, and pairing it with the correct shackle, thimble or turnbuckle decides whether the strength you paid for actually reaches the load. In this guide I’ll walk you through every common termination and fitting, with the efficiency numbers, installation rules and inspection points I use when specifying assemblies for customers.
Why the Termination Is Often the Weakest Link
When a wire rope passes around a radius and gets terminated, the rope’s load paths change. In a swept-back eye or a socket cone, the wires are no longer perfectly aligned, bending stresses concentrate at the throat, and some of the rope’s catalogue strength is always surrendered. Termination efficiency is the number that tells you how much you keep: the measured breaking strength of the finished assembly, expressed as a percentage of the bare rope’s minimum breaking load (MBL). If a socketed assembly breaks at 100% of catalogue and a clipped eye breaks at 80%,
The arithmetic matters at lift-planning level. Usable capacity equals the rope’s MBL, multiplied by the termination efficiency, divided by the design factor. At a 5:1 design factor — the norm for slings, as I explain in my guide to the wire rope sling safety factor — a 100% termination leaves 20% of catalogue strength as working capacity; an 80% termination leaves 16%. And note the fine print: published efficiencies only hold when the termination is made correctly. A badly fitted clip does not hold at “a reduced rating” — it holds at whatever the mistake left you, and nobody has measured that.
The Main Wire Rope Termination Types
Terminations fall into two families: permanent terminations (sockets and swaged fittings, made once and kept for the rope’s life) and field or re-usable terminations (clips and wedge sockets, which can be applied on site and undone). Here is how each behaves in practice.
Spelter Sockets (Zinc or Resin Poured)
The spelter socket is the benchmark: broom the rope end, insert it into a conical basket, and fill the void with molten zinc or a two-part resin. Under load the cone wedges the wires into the socket, gripping every wire evenly — a properly poured socket develops 100% of the rope’s MBL with minimal elongation and excellent fatigue behaviour. Zinc pours demand heat control (and are best done in the shop); resin sockets need no heat, tolerate site conditions better, and reach full strength after curing — which makes them the standard choice for offshore and field work on crane pendant lines, bridge stays and mooring systems. The trade-offs: it is permanent, it needs clean, degreased wires inside the basket, and the broomed end cannot be reused.
Swaged Sockets, Terminals and Ferrules
Swaging cold-forms a steel or aluminium sleeve around the rope end under enormous hydraulic pressure, flowing the sleeve metal into the gaps between outer wires. Solid swaged sockets and threaded terminals reach 100% efficiency; swaged-sleeve eye loops (Flemish eyes and turnback eyes) typically achieve 90–95%. Swaging is strictly shop work — the presses do not travel — which is precisely why field options exist. The result is compact, clean and permanent — which is why swaged terminals dominate structural cable systems and volume sling production.
Mechanical Spliced Eyes (Flemish Eye with Swaged Sleeve)
The standard crane and sling industry eye: the rope is divided into its strand groups, passed around a thimble, and the tails are locked under a press-formed sleeve. Done correctly it is elegant — the load path stays symmetrical and efficiency is 90% or better on smaller diameters, tapering slightly on large ropes. Almost every wire rope sling you buy is built this way.
Hand-Tucked Eyes
The traditional spliced eye, strands hand-tucked around a thimble. Efficiency depends on diameter — roughly 90% at 6 mm falling to about 80% on large ropes. Still seen on small general-purpose slings, but largely displaced by mechanical splices.
Wire Rope Clips (U-Bolt Clips with Thimble)
Clips are the field-terminable workhorse — and the most misused fitting in rigging. Correctly installed (right number, right spacing, correct orientation, correct torque) they hold about 80% of rope MBL. The classic rule is “never saddle a dead horse”: the saddle (bridge) of the clip must bear on the live end — the load-carrying part of the rope — and the U-bolt must press on the dead end. Saddle the dead end and you crush the load-bearing strands at exactly the point of highest stress — the single error that recurs through decades of accident reports.
Wedge Sockets
A grooved wedge and tapered housing grip the rope by geometry: tension on the live end pulls the wedge deeper. Efficiency is about 80%, but the fitting is re-usable and adjustable in the field, which makes it the standard rope anchor on mobile crane winches, draglines and excavator hoists where ropes are changed frequently. The dead end must be secured (a clip below the socket is the usual arrangement) so the wedge cannot back out if tension momentarily releases. One caution from experience: wedge sockets are generally not recommended for rotation-resistant rope constructions.
The table below is the one I sketch whenever a customer asks which termination to buy. Bands assume the manufacturer’s procedure is followed exactly:
| Termination | Efficiency | Made where | Re-usable? | Typical duty |
|---|---|---|---|---|
| Spelter socket, zinc pour | 100% | Shop preferred | No | Pendant lines, stays, mining, heavy permanent anchors |
| Spelter socket, resin | 100% | Shop or field | No | Offshore, mooring, site socketing where heat is unwanted |
| Swaged solid socket / terminal | 100% | Shop only | No | Structural and architectural cables, permanent fittings |
| Flemish eye + swaged sleeve | 90–95% | Shop only | No | Volume-produced wire rope slings |
| Hand-tucked eye + thimble | 80–90% (by diameter) | Shop | No | Small general-purpose and marine slings |
| Wire rope clips + thimble | ~80% | Field | Yes | Temporary attachments, guys, low-duty static lines |
| Wedge socket | ~80% | Field | Yes | Mobile crane, dragline and excavator rope anchors |
The Hardware Around the Rope: Shackles, Thimbles, Turnbuckles
A termination rarely works alone — the hardware it connects through is often the true limiting link. These are the fittings I check on every assembly drawing:
Shackles
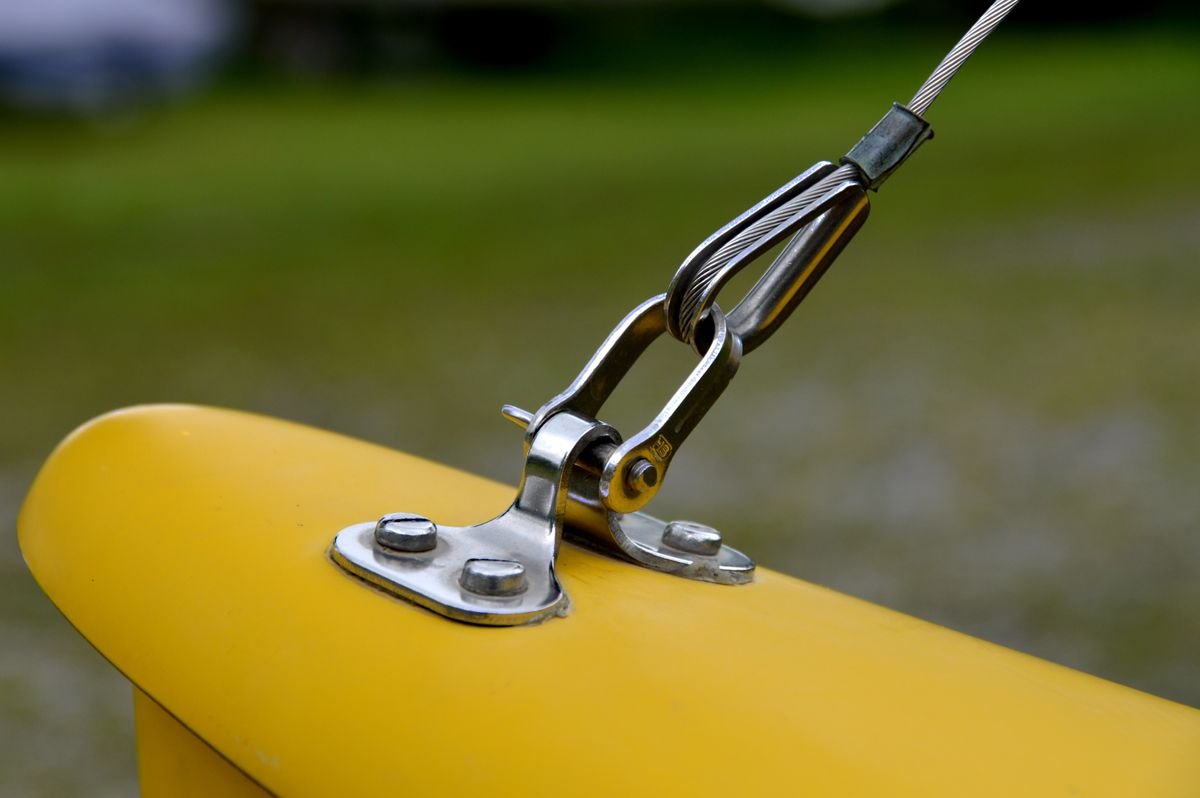
Bow (anchor) shackles accept multi-leg slings and side loading better; dee (chain) shackles are more efficient for in-line pulls. The working load limit is marked on the bow — never infer it from pin diameter. Two habits prevent most shackle failures: never side-load a bow shackle without de-rating per the manufacturer, and always seat the pin fully — screw-pin shackles where vibration is absent, bolt-type (safety) shackles with nut and cotter wherever the pin could back out. Standards to specify against: EN 13889 or ASME B30.26.
Thimbles
A thimble is a cheap insurance policy for the eye. It maintains the eye’s radius, keeps the rope from crushing flat, and can multiply eye life many times over in cyclic service. Light-pattern thimbles suit static lines; heavy-pattern (deep groove, thick section) belong on slings and mooring lines where the eye works over a shackle. Match the thimble to the rope diameter and the pin it will ride on.
Turnbuckles
Open-body turnbuckles (jaw-jaw, eye-eye or jaw-eye) adjust tension in stays, guys and lashing systems. Two details decide their service life: a locking provision (lock nuts or lock wire) so vibration cannot unwind them, and full thread engagement before the assembly is loaded. Specify forged bodies to DIN 1480 or the ASME equivalent — and remember a turnbuckle is a tensioning device, not a lifting hook.
| Fitting | Function | Key standard | Selection tip |
|---|---|---|---|
| Shackle, bow type | Connects slings to loads and anchors; accepts multi-leg, slight side loads | EN 13889 / ASME B30.26 | De-rate heavily for side loading; prefer bolt-type pins on vibrating rigging |
| Shackle, dee type | In-line connection, most efficient geometry | EN 13889 / ASME B30.26 | WLL is marked on the bow — never guess from pin size |
| Thimble | Protects and shapes the rope eye; prevents crushing | DIN 3090 | Heavy pattern for slings and mooring; match to rope dia and bearing surface |
| Turnbuckle | Adjusts tension in stays, guys and lashings | DIN 1480 | Full thread engagement plus lock nuts; never use as a lifting point |
| Wire rope clip | Field-made eye termination | EN 13411-5 / ASME B30.26 | Saddle on the live end; correct count, spacing and torque (table below) |
| Spelter / wedge socket | Permanent or field rope anchor | EN 13411-6 / API specs | Resin for field work; secure wedge-socket dead ends; avoid wedges on rotation-resistant ropes |
Installation Rules That Decide Whether the Rating Is Real
Most termination failures I review trace back to installation, not the fitting itself. The rules that matter most: For clips, apply the correct number with correct spacing (typically 6 rope diameters apart), torque them with a calibrated wrench, and — critically — re-torque after the first significant loading, because the strands bed in and the rope settles. For resin sockets, degrease the broomed wires completely and respect the cure time before loading; a resin pour loaded early will creep. For wedge sockets, seat the rope fully into the wedge groove and secure the tail. And for every termination type, mind the D/d ratio: a bearing surface too small for the rope diameter steals strength no clip count can recover.
| Rope diameter | Minimum clips | Minimum turnback (eye) length | Typical torque (carbon steel clips) |
|---|---|---|---|
| 6–8 mm | 2 | 250 mm | 15–30 N·m |
| 9–13 mm | 3 | 450 mm | 60–80 N·m |
| 14–16 mm | 3 | 500 mm | 80–100 N·m |
| 18–20 mm | 4 | 700 mm | 120–150 N·m |
| 22–26 mm | 4 | 850 mm | 180–220 N·m |
| 28–32 mm | 5 | 1,050 mm | 270–330 N·m |
| 36 mm and above | 6 | 1,200 mm | 400 N·m and above |
Treat the table as orientation only — the clip manufacturer’s own table (per EN 13411-5 or ASME B30.26) always governs.
Inspection and Discard: Watching the Rope Ends
Terminations age, and they age differently from the rope body. On clipped eyes, look for loosened nuts (re-torque is a maintenance task, not a one-off), thimble groove wear and corrosion where the rope enters the eye. On wedge sockets, check that the wedge has not backed off and the dead-end tail is still secured. On sockets and swaged fittings, check the body for cracks, the collar for slippage, and the rope immediately behind the termination — fatigue breaks cluster in the last metre before a socket, where bending is constrained. All of this folds naturally into the rope inspection regime: my guide to ISO 4309 inspection and discard criteria covers the rope body, and the same inspection walk should include the terminations and their hardware. A loose or cracked termination is not a condition to monitor — it is an immediate removal from service.
Choosing the Right Termination: My Recommendations by Application
Two decades of specifying assemblies have taught me that the “best” termination is the one matched to duty, environment and who has to make it. My default recommendations:
| Application | My recommendation | Why |
|---|---|---|
| Mobile crane / excavator hoist rope end | Wedge socket with secured tail | Field-adjustable, fast rope changes; ~80% is acceptable at the dead end |
| Sling eyes, serial production | Flemish eye + swaged sleeve (heavy thimble) | 90%+ efficiency, consistent quality, economical at volume |
| Pendant lines, guy stays, bridge hangers | Spelter socket (zinc shop pour) or swaged terminal | 100% efficiency, minimal elongation, fatigue-resistant |
| Offshore / mooring terminations | Resin-spelter socket | No hot work on deck; full strength after cure |
| Temporary rigging and site repairs | Wire rope clips on thimble, correctly torqued | Only re-usable field option; inspect and re-torque after first load |
| Structural and architectural cables | Swaged threaded terminals | Compact, precise adjustment, clean appearance |
The Bottom Line From a Rope Specialist
If you remember three things from this guide, make them these: match the termination to the duty; install it exactly to the manufacturer’s procedure, because every efficiency number assumes you did; and inspect terminations with the same discipline as the rope body. When a lift really matters, buy the rope and terminations as one certified assembly, with the breaking load tested as a complete unit. Aulone is a professional manufacturer and supplier of steel wire ropes, wire rope slings, synthetic ropes and rigging hardware for lifting, marine, mining, construction and industrial applications. With more than 20 years in the industry, an annual capacity of 200,000 tons, and EN 12385-4 certification, ISO 9001 quality management, class approvals including BV, ABS, DNV and RMRS plus CE marking, we build custom socketed, swaged and spliced assemblies from stock rope, with third-party testing on request. If you are unsure which termination your application needs, send the duty details to info@wireropes.net and I will help you specify it.
FAQ: Wire Rope Terminations and Fittings
How much strength do you lose with wire rope clips?
Correctly installed clips develop about 80% of the rope’s minimum breaking load. Incorrect installation — saddling the dead end, too few clips, wrong torque, no re-torque after loading — can push efficiency far below that, which is why clips are reserved for temporary and low-duty applications rather than critical overhead lifts.
What does “never saddle a dead horse” mean?
It is the mnemonic for clip orientation: the saddle (the bridge over the U-bolt) must rest on the live end — the load-carrying rope — and the U-bolt presses only on the dead (short) end. Put the saddle on the dead end and you crush and fatigue the wrong side, which has featured in decades of accident reports.
Zinc or resin for a spelter socket — which is better?
Both develop 100% efficiency when done properly. Zinc pours are the traditional shop method with excellent fatigue behaviour but need molten metal and heat control. Resin socketing needs no heat, is more forgiving of field conditions, and is therefore the default offshore and on-site choice — provided the wires are degreased and the cure time is respected before loading.
How many wire rope clips do I need?
As a guide: 2 clips up to 8 mm rope, 3 clips for 9–16 mm, 4 for 18–26 mm, 5 for 28–32 mm, and 6 above 36 mm, spaced about six rope diameters apart with the specified turnback length. Always follow the clip manufacturer’s table per EN 13411-5 or ASME B30.26 — counts and torques vary by brand and clip style.
Can a wedge socket be used for lifting?
Yes — at roughly 80% efficiency it is the standard rope anchor on mobile crane and excavator hoists. Seat the rope fully in the wedge, secure the dead-end tail so the wedge cannot back out, and note that many manufacturers advise against wedge sockets on rotation-resistant ropes — check with your rope supplier.
How often should terminations be inspected and re-torqued?
Inspect terminations at every routine rope inspection — and re-torque clipped eyes after the first significant loading and periodically thereafter, because strands bed in and the eye settles. Socketed and swaged fittings need visual checks for cracks, collar movement and the rope immediately behind the termination. Any fitting found cracked, loose or slipping comes out of service immediately.